
“We inspect to AQL” is not a complete power-tool quality plan. Acceptance sampling can guide a decision about a defined lot, but the buyer still has to say what constitutes a defect, which product variants are in the lot, what tests are permitted and what happens after a failed sample. It does not guarantee that every uninspected unit is conforming. For powered products, a buyer should combine a defensible sampling plan with clear configuration control, factory process checks and appropriate product-specific safety evaluation.
This article is a practical framework for importers and private-label brands preparing a pre-shipment inspection. It does not supply a universal defect limit, a certification of any tool, or a substitute for the buyer's contract and qualified compliance advice. The terms and plan need to be agreed before production is finished, not negotiated beside pallets while a vessel booking is imminent.
Define the lot before selecting a sample
A lot should be coherent enough that a sample says something useful about the goods being evaluated. If one shipment contains several drill models, two charger plug variants and multiple carton languages, treating everything as one undifferentiated lot can conceal a market-specific error. Define the inspection unit by SKU, production batch or other appropriate boundary and explain how mixed cartons will be handled. Record lot size and where the goods will be accessible for random selection.
Do not allow the factory to present only the cleanest cartons. The inspector needs access to the entire eligible lot and a method for selecting units without bias. If the goods are still being packed, agree whether the inspection is in-process or truly pre-shipment. A result from 60% of finished goods cannot automatically be applied to the remaining 40% if the process or components change.
The American Society for Quality describes ANSI/ASQ Z1.4 as an attribute-sampling system with plans and switching rules. AQL means acceptance quality limit in that context; it is not permission for a factory to intentionally ship a fixed percentage of defects. The correct table, level and rules should be selected by a competent quality professional for the contract. Do not copy a random “standard AQL” number from another product category.
Caption: A sampling result depends on a defined lot, defect list and access to all eligible goods.
Classify defects in terms a buyer can act on
Write a model-specific defect list with examples and photographs. A wrong mains plug, missing guard, damaged insulation, incompatible battery or safety-warning omission may carry a different consequence from a minor cosmetic mark, but the classification must be agreed by qualified parties and relevant requirements. Avoid universal “critical/major/minor” labels without saying how the exact product and market were assessed.
Include functional and documentary checks. For an angle grinder, the guard, handle, switch, wheel interface, nameplate and carton contents deserve attention. For a chainsaw, the bar and chain, controls, oil-system parts and manual are central. For a cordless drill, battery and charger identity are part of the inspected unit. For a planer, blade type and setting information matter. The general quality-control checklist can be tailored to these specific SKUs.
Agree what counts as one defective unit if several flaws appear on it and how repeated defects are counted. The inspector should not have to interpret a vague phrase such as “acceptable appearance” under deadline pressure. Provide an approved sample or photographs, a version-controlled specification, permitted test method and escalation contact. A defect sheet with a few dozen practical examples is more valuable than a long certificate folder unrelated to the shipment.
Choose checks that sampling can reasonably support
Visual, dimensional, accessory-count and non-destructive function checks can often be included in a pre-shipment plan. Some safety or endurance tests require specialized equipment, more time or destructive methods; these may belong in design qualification, component testing or factory process controls rather than a quick carton-side inspection. The buyer should state which evidence is expected before shipment and which checks are not part of the inspector's task.
For each function check, define the setup: supply or battery, accessory, duration, pass/fail criterion and safe work area. An inspector should not improvise a grinder test with an unapproved disc or a chainsaw test on loose scrap wood. If a test requires an engineer, laboratory or trained operator, assign it explicitly. The acceptance-sampling framework only tells the team how to decide from observed results; it does not make an unsafe or invalid test acceptable.
ASQ's acceptance-sampling explanation distinguishes attribute observations from measured variables. A buyer may need both: count damaged cartons, but measure a critical dimension where appropriate. The plan should say how each measurement is made and whether the instrument is suitable. “AQL passed” without the underlying observations gives little learning for future production.
Mid-article sourcing CTA: Preparing a power-tool inspection? Send your models, market variants and proposed defect list to discuss a shipment-ready specification.
Connect inspection to earlier approvals
Pre-shipment inspection confirms an approved configuration; it cannot create one. Before production, the buyer should have signed off the tool, accessories, labels, manuals and retail packing. The sample-approval guide describes that earlier step. If the factory substitutes a charger or blade after sample approval, the inspector needs a documented decision on whether the change is accepted and what claim or conformity review was performed.
Factory testing and process checks also matter. A final sample may fail because of a systematic assembly issue that should have been detected earlier. Conversely, a passed sample does not prove that no sporadic issue exists in the lot. Ask for the factory's process records relevant to the selected model, then use the pre-shipment visit as a final cross-check. This avoids the false belief that a single inspection can “add quality” to goods already packed.
The product's traceability code should link inspected cartons to the lot and production record. If a failure appears later, the buyer needs to know which batch was sampled and what was observed. The lot-traceability guide covers this connection.
Decide the action before the result arrives
Write the decision path: pass, fail, hold, rework, re-inspect or escalate to engineering and compliance. Specify who can approve a deviation and whether freight booking is paused. A repeated wrong-plug problem cannot be solved by simply increasing the number of cosmetic checks. The factory should identify affected stock, correct the cause and provide evidence before the buyer considers release.
If the lot fails, do not automatically ask for a second sample until the first result disappears. A re-inspection should follow an agreed corrective action and, where necessary, revised sampling logic. Keep both reports. If the issue concerns safety or regulatory information, consult qualified specialists; a commercial acceptance decision cannot waive legal obligations.
Inspect export packing after any rework. A unit may be corrected but placed into a damaged or wrong-language carton. The final report should identify the inspected lot, sample selection, checks, defects, photographs, disposition and any open questions. “Passed AQL” is a summary, not the full decision record.
Keep the inspection commercially useful
Compare results across orders. Recurring minor defects may not stop one shipment but can erode retailer confidence and consume service time. A high rate of missing accessories may indicate a packing-process issue. A cluster of function failures in one shift may point to incoming parts or a test fixture. Use the observations to improve the next production run, not merely to negotiate a price deduction.
Avoid publishing a claim that ToolViron “guarantees zero defects” because a sample inspection was passed. The credible statement is narrower: a model-specific plan was agreed, checks were recorded, and any issues were handled under the contract. The manufacturing page can provide factory context, but the purchase order and approved specification determine what a particular shipment must meet.
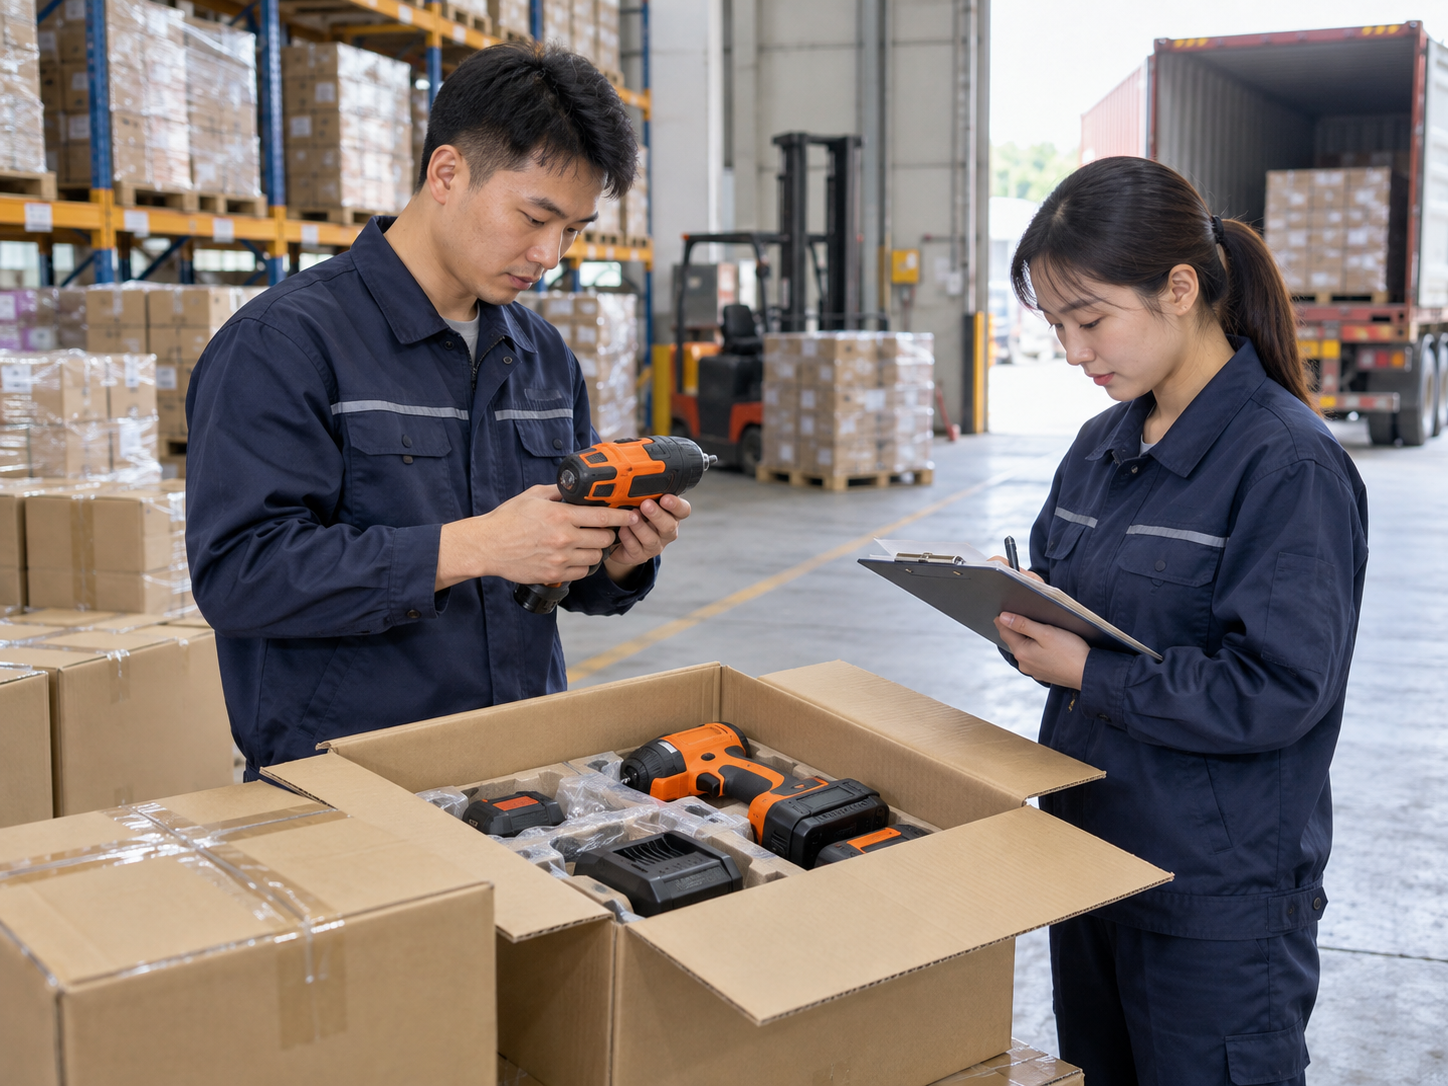
Caption: Illustrative shipment photography: every order needs its own approved inspection record.
A worked inspection-planning example
Suppose an importer orders a mixed container of corded drills and cordless drill kits for two markets. One kit uses a different charger plug and manual language. If the buyer says “inspect the container at AQL,” the inspector may sample mostly one variant and miss a systematic wrong-plug error in the other. The buyer should define separate lots or stratified checks that address each SKU and market configuration. The exact sampling method belongs in the approved inspection plan, but the principle is simple: the inspected population must match the decision being made.
For each variant, prepare a defect list and an approved packed sample. A wrong charger plug is not a cosmetic scratch; it can make a product unsaleable and may raise safety or compliance concerns. A missing bit set, damaged case and slight paint mark are different problems. Qualified product and compliance staff should classify them before inspection. The inspector records observed facts and applies the agreed criteria, rather than inventing a severity judgment beside the goods.
Ask the factory when all units will be finished and accessible. If one market variant is still awaiting manuals, the inspector should not declare that portion passed based on the completed variant. If rework occurs, identify the affected cartons and the method for verifying correction. A failed inspection report should remain in the file even after the lot later passes a repeat visit. It explains what changed and whether the root cause was addressed.
The buyer may also request a few safe functional checks. Define the battery, bit, material and duration for the drill test. A generic instruction to “test function” can produce inconsistent observations and unsafe improvisation. For any product-safety test requiring special equipment, refer to the earlier qualification or factory records and assign a qualified reviewer. The pre-shipment inspector's sampling visit is not a substitute for the product's design assessment.
How to use results after goods are released
Inspection data should guide the next order. If several lots show repeated missing accessories, the packing line needs an in-process check. If a defect appears only in one plug variant, review segregation and labelling. If cosmetic damage rises after a new carton insert, the packaging change may be the cause. These trends are useful even when individual lots passed their acceptance decisions. Treat inspection as a feedback system, not only a release stamp.
The buyer should also compare customer complaints with the inspection record. A defect not seen in the sample can still exist in the lot; sampling has limits. If several reports point to one batch, investigate the factory records and hold affected unsold stock if warranted. A passed AQL report is evidence of the agreed sample decision, not a defence against all later information. The traceability code helps locate the goods involved.
Document the decision owner. Purchasing may manage schedule and cost, but engineering and compliance should review safety-related findings. No one should waive an unknown electrical or guarding issue solely to catch a vessel. The contract should state who can accept deviations, whether rework is allowed, what evidence is needed and whether a third-party re-inspection is required. This prevents a high-pressure shipping day from becoming the moment when quality policy is invented.
Finally, give the factory constructive defect feedback with photographs, part numbers and lot information. “Failed AQL” alone does not tell an assembly team what to correct. Specific observations make corrective action possible and allow the buyer to verify that the next shipment is genuinely improved.
One decision the inspector should never have to improvise
The inspector may encounter a defect absent from the agreed list, such as a charger with unfamiliar markings or a wheel accessory packed without its protective guard. The plan should name an escalation contact and a hold rule for unexpected safety or conformity concerns. It should not instruct the inspector to classify every unknown issue as minor to preserve the shipping schedule. Photographs, unit and lot identifiers, and the exact product configuration should be sent to the responsible buyer team. The decision can then be made by people with the relevant engineering and market knowledge, documented in the report and applied consistently across the affected stock.
Frequently asked questions
Does passing AQL mean there are no defective tools in the shipment?
No. Acceptance sampling makes a lot decision from a sample under stated assumptions; uninspected units are not individually proven conforming. Process control and product-specific tests remain important.
Can one AQL plan cover multiple SKUs and markets?
Not automatically. Different product configurations and market variants may need separate lot boundaries or checks. Define the population before choosing the sample.
Who should classify a missing guard or wrong plug?
The buyer's qualified quality and compliance team should define classifications for the exact product and market before inspection. An inspector then applies the approved list and escalates unexpected findings.
What happens after a failed inspection?
Hold release, document defects, identify affected stock, agree corrective action and re-inspection rules, and retain both reports. Safety or conformity concerns need specialist review rather than a simple commercial waiver.
Conclusion
AQL can support power-tool pre-shipment decisions only when the lot, defects, sample method and disposition are defined. It is not a quality guarantee or a substitute for good sample approval and factory testing. Give the inspector the exact configuration, safe methods and decision authority needed to produce a report the buyer can act on.
Send your requirements
Share the tools, SKUs, destination markets and inspection concerns. ToolViron can discuss the information needed for a model-specific shipment-check plan. Send your requirements to begin.
Images illustrate product and inspection topics; they are not documentary evidence of a specific ToolViron test or customer project. Confirm the exact model and market requirements before ordering.